Successful pcb fabrication and assembly depends on more than a clean schematic. Material choice, layout details, and assembly controls all affect whether a board performs reliably. A small footprint error can complicate soldering, while an unclear drawing may lead to avoidable questions on the production floor.
The most useful checks happen before files reach a supplier. Confirm component availability, copper weights, board thickness, hole sizes, and spacing against the intended process. Review the bill of materials for accurate part numbers and acceptable alternatives. In production, teams often find that a brief design-for-manufacturing review catches issues that look harmless on screen. Details matter. Still, no checklist can predict every problem; prototypes sometimes reveal heat, fit, or signal issues that design reviews miss.
These ten tips focus on practical decisions across fabrication, assembly, and inspection. They cover clear documentation, suitable materials, panelization, solder paste, component placement, and functional testing. Each step helps reduce ambiguity between design intent and the finished board. A capable manufacturer can offer valuable process guidance, but the design team should verify critical requirements rather than assume every detail is understood. The goal is not perfection on the first try. It is a repeatable process, supported by measured checks and thoughtful revisions when results fall short.
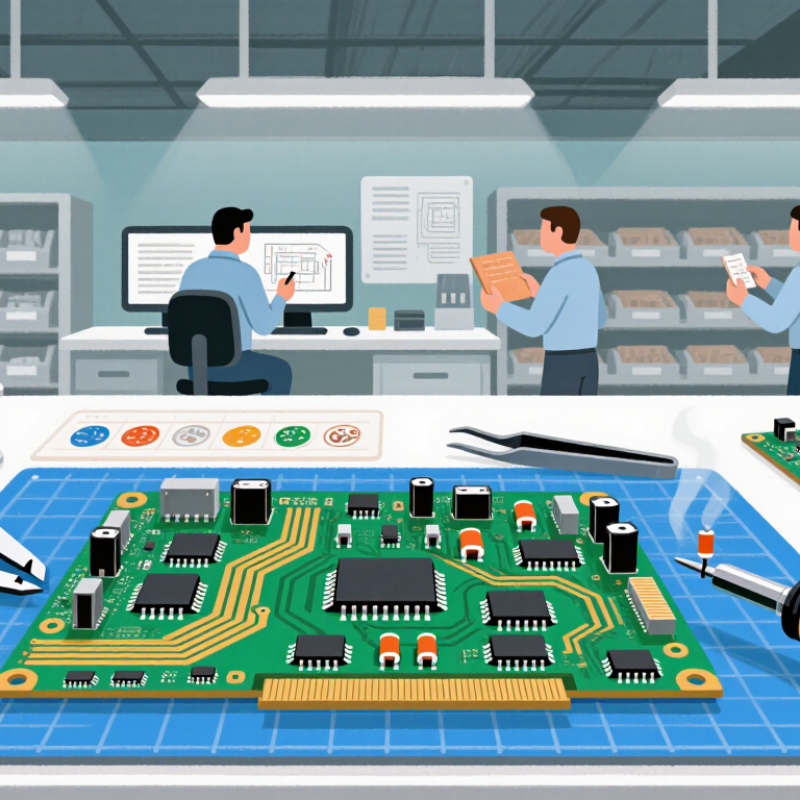
A reliable PCB build starts with clear electrical and mechanical requirements. Specify the board outline, layer count, copper weight, finished thickness, and minimum trace and spacing dimensions. Describe the operating environment, including expected temperature, vibration, and moisture. Give the assembler connector locations, component orientation, and any keep-out zones. Small omissions matter.
Production constraints shape what can be built consistently. Set acceptable tolerances for holes and board dimensions, and identify controlled-impedance nets when signal performance depends on them. Share the bill of materials, approved component substitutions, and expected production quantity early. Ask your fabricator and assembler to flag limits before design release. A tight via size or unusual component spacing may affect yield, lead time, or inspection. Even a careful checklist can miss a constraint; review it with the people who will build the board.
Tips: Keep one dated requirements document. Mark critical dimensions clearly on the drawing. Confirm that footprints match the actual component datasheets. If a requirement is negotiable, label it as such. Then request a design-for-manufacturing review and resolve open questions before ordering. A quick email is not enough for a disputed tolerance.
A reliable PCB layout starts with the fabricator’s actual capabilities, not a generic rule set. Before routing, confirm minimum trace and space, finished-hole tolerances, copper weights, and the layer stackup. These details affect whether a board can be produced consistently. Keep critical dimensions comfortably within stated limits; designs close to process boundaries leave less room for variation. Ask about recommended annular-ring and solder-mask clearances, too. Small gaps matter.
Give high-current paths enough copper width, and keep return paths continuous beneath fast signals where possible. Avoid routing across plane splits, which can create unwanted return-current detours. Place vias clear of pads unless the process specifically supports via-in-pad construction. Check connector locations against the board outline and mounting hardware. Leave room. A few millimeters can prevent a connector shell from colliding with a screw or enclosure wall.
Use consistent footprints and verify pad dimensions against component drawings. Add clear polarity marks, accessible test points, and fiducials where assembly requires them. It is tempting to pack in one more component, but that choice deserves a second look. A dense layout may appear tidy on screen while leaving too little space for soldering or inspection. Run a design-for-manufacturing review before release, then revisit any suggested changes with the fabricator; some recommendations may require a layout tradeoff.
Example PCB layout design-rule starting points (mm)
These practical starting points can help improve manufacturability. Actual limits vary by board material, layer count, copper weight, and fabrication process, so confirm the final rules with your PCB manufacturer.
Material selection should follow the board’s operating conditions, not just the default used on an earlier project. For a low-speed control board in a stable indoor environment, standard FR-4 may be adequate and economical. Boards exposed to repeated heat cycles may need a higher glass-transition temperature. High-speed or RF designs can require a laminate with carefully controlled dielectric properties. Check the actual signal, temperature, and moisture requirements before choosing. Small details matter.
Board specifications should describe the stack-up, finished thickness, copper weight, minimum trace and spacing, hole sizes, and any controlled-impedance requirements. These details affect both manufacturability and cost. A tight spacing limit may be unnecessary if the layout can be adjusted, while undersized drill requirements can constrain via choices. Share the draft stack-up and critical dimensions with the fabricator before the layout is frozen; their process limits can reveal problems early. Leave room to adjust. It is tempting to specify every feature at the tightest possible tolerance, but that can add cost without improving function. Review which dimensions truly affect performance, and allow practical tolerances elsewhere.
Coordinating PCB fabrication with component assembly means managing one shared production plan. A bare board may arrive on time yet miss its assembly slot if components, stencils, or approved files are late. Small gaps matter. McKinsey’s 2022 report, Taking the pulse of shifting supply chains, found that 45% of surveyed companies had no visibility beyond their tier-one suppliers. That broader supply-chain finding applies to PCB planning, too: teams need clear status for parts and process steps, not just board delivery dates.
Before release, align the fabricator and assembler on the same revision, stackup, surface finish, panel layout, and delivery quantity. Send a complete, matching package: fabrication data, drill files, bill of materials, pick-and-place coordinates, and assembly drawings. Confirm component availability early, and document any approved substitute. A BOM can feel final, but shortages may change it; uncontrolled substitutions can create footprint, polarity, or qualification problems. Ask the assembler to review pad geometry and stencil needs before the board is built. That review may expose issues, though it cannot guarantee a defect-free run.
Tips: Share a dated milestone plan. Freeze revisions before tooling. Track long-lead parts weekly. Label sample boards clearly, and compare the first assembled unit against the latest approved files. Keep one owner for change control. One detail is easy to miss: a schedule update means little unless both suppliers receive it.
Inspection begins before power is applied. Under bright, angled light, check for solder bridges, lifted pads, skewed components, and residue around fine-pitch parts. A magnifier helps, but it cannot reveal every hidden joint. For dense boards, automated optical inspection can flag placement and solder-shape issues; X-ray inspection may be needed for joints beneath packages such as BGAs. Neither replaces engineering judgment. Compare component polarity and reference designators against the assembly drawing, especially near connectors and polarized capacitors. Small orientation errors are easy to miss.
Testing should move from low risk to full function. With power off, use a multimeter to check for unintended shorts between supply rails and ground. Then apply power through a current-limited supply, watching current draw and hot spots. Slowly. Verify key voltages at test points before running firmware or connecting external equipment. Functional checks should exercise real inputs and outputs, not just confirm that the board boots. Record test limits, readings, and failures so recurring defects can be traced to a process step. A cold joint can pass a brief bench check, then fail when a connector is flexed. That deserves a second look.