Choosing among the 2026 top board assembly manufacturers requires more than comparing website claims. Global buyers need evidence of stable production, transparent quality controls, and dependable communication.
This guide examines manufacturers through practical factors. These include engineering support, component sourcing, prototype speed, production capacity, and shipment consistency. A capable partner should explain its DFM process clearly. It should also provide inspection records, traceability data, and realistic lead-time estimates. AOI, SPI, and X-ray inspection can reveal hidden soldering problems. However, equipment alone does not guarantee reliable results. Experienced technicians and disciplined process control still matter.
Quality certifications, such as ISO 9001 or relevant IPC practices, can strengthen confidence. They should support real procedures, not decorate a sales page. Buyers should request sample reports, factory details, and references for similar products. A medical controller, industrial sensor, and consumer device require different risk controls. Cost matters, but the lowest quotation may create delays, rework, or difficult communication later.
No ranking remains perfect for every buyer. Capacities, certifications, staffing, and supply conditions can change during 2026. Some manufacturers may excel at prototypes but struggle with complex volume production. Others may offer strong board assembly services while providing limited design guidance. This guide therefore presents useful comparisons, not permanent verdicts. Verify current capabilities before signing a contract. Ask specific questions. Inspect the details. A careful evaluation can turn a promising supplier into a reliable long-term manufacturing partner.
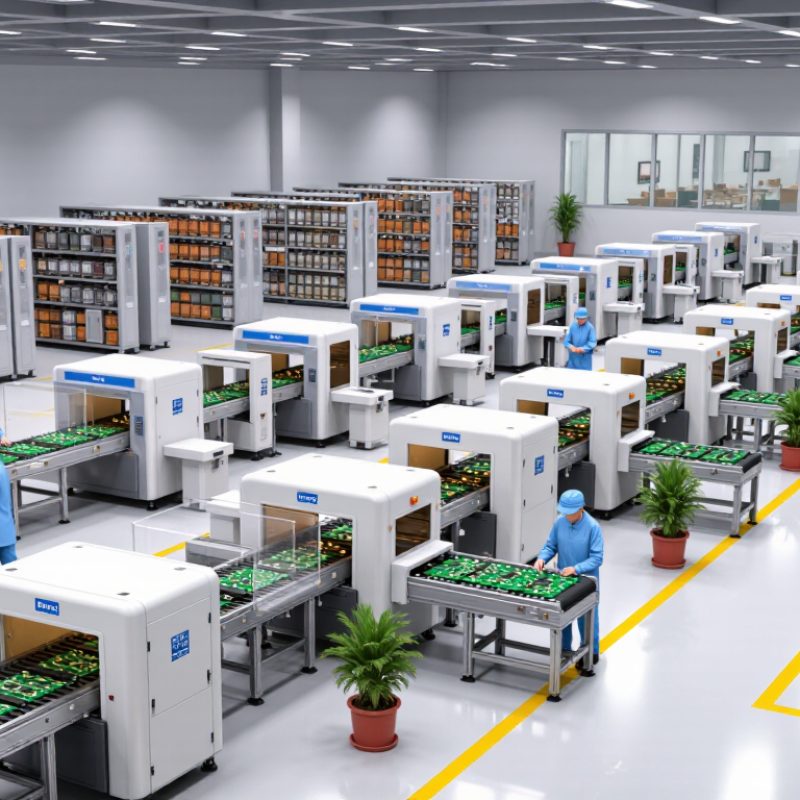
Board assembly manufacturers turn circuit designs into tested, usable electronic boards. Their work often includes component sourcing, printed circuit board preparation, surface-mount placement, through-hole assembly, soldering, and final inspection. They may also support design-for-manufacturing reviews before production begins. This step can reveal weak solder joints, crowded components, or parts that are difficult to replace.
Global buyers need these manufacturers because production involves more than placing components. Experienced teams use automated optical inspection, X-ray inspection, electrical testing, and process records to control quality. They can provide lot tracking, approved component lists, packaging protection, and export documentation. These details matter when boards travel through different climates and supply networks. A reliable manufacturer also explains lead times clearly and reports material changes before they affect production.
Clear communication matters.
Very much.
Buyers should review quality certificates, testing methods, sample results, and factory procedures before placing large orders. In my experience, a clean inspection report does not prove a perfect process. Human review can miss unusual defects, especially during rushed production. Buyers should ask how errors are corrected, not only how they are prevented. A capable assembly partner shares evidence, accepts reasonable audits, and adjusts its process when field feedback exposes a weakness. That honesty is sometimes more valuable than a polished sales presentation.
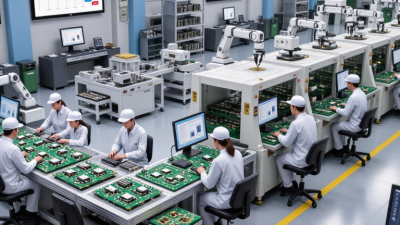
For global buyers, board assembly capability means more than placing components quickly. It covers engineering support, production control, testing, and dependable communication. Ask whether the manufacturer reviews Gerber files, bills of materials, and assembly drawings before quoting. A capable team should identify missing tolerances, unclear polarity marks, or parts with long lead times. Practical experience matters. Request examples of similar board sizes, component densities, and production volumes.
Quality standards must be visible on the factory floor. Check certification records, calibration dates, operator training, and inspection procedures. Automated optical inspection can detect misplaced parts and solder bridges. X-ray inspection helps examine hidden joints under bottom-terminated components. Reflow profiles should be recorded for each approved solder paste and board design. Traceability should connect each board to material lots, machine settings, inspection results, and repair records. Ask for actual defect data, not only polished presentations.
No factory is flawless. The useful question is how quickly it detects and corrects mistakes. A strong supplier explains its corrective-action process without avoiding uncomfortable details. Review sample first-article reports and ask how design changes are controlled. Visit the production area when possible. Look for labeled materials, clean workstations, controlled storage, and consistent documentation. One weakness deserves attention: some suppliers meet formal standards but communicate poorly during schedule pressure. Test that relationship before a large order, because silence can become an expensive quality problem.
| Evaluation Dimension | What to Verify | Recognized Benchmark or Standard | Practical Evidence to Request | Suggested Weight | Buyer Priority |
|---|---|---|---|---|---|
| Quality Management System | Documented procedures for purchasing, production, inspection, nonconformance control, corrective action, and continual improvement. |
ISO 9001:2015 A sector-specific quality system may also be required for regulated industries. |
Current certificate, certification scope, issuing body, latest audit status, corrective-action records, and quality objectives. | 15% | Critical |
| Soldering and Assembly Workmanship | Ability to produce consistent through-hole, surface-mount, mixed-technology, and lead-free assemblies. |
IPC J-STD-001
IPC-A-610 Confirm whether the program requires IPC Class 2 or the more demanding Class 3 acceptance level. |
Operator and inspector training records, process qualification documents, sample inspection reports, and representative finished assemblies. | 15% | Critical |
| Surface-Mount Technology | Placement accuracy, component range, fine-pitch capability, double-sided assembly, package handling, and line changeover control. | Capability should be demonstrated against the buyer’s actual bill of materials, package mix, board dimensions, and density requirements rather than by machine count alone. | Equipment list, nozzle and feeder range, placement capability data, defect-per-million or first-pass-yield records, and a sample production traveler. | 12% | Critical |
| Process Control and Inspection | Control of solder paste deposition, reflow profiles, component orientation, solder joints, polarity, and assembly defects. | Typical control methods include solder-paste inspection, automated optical inspection, X-ray inspection for hidden joints, and documented reflow profiling. | Inspection coverage map, sample SPI/AOI/X-ray images, calibration certificates, process-control plans, and defect Pareto reports. | 12% | Critical |
| Traceability and Material Control | Ability to trace components, lot codes, date codes, operator actions, machine parameters, inspection results, and finished-unit serial numbers. | Traceability depth should be defined contractually according to product risk, regulatory requirements, and field-service needs. | Mock traceability report, material receiving records, barcode system demonstration, lot-control procedure, and retention-period policy. | 10% | High |
| Component Sourcing and Counterfeit Prevention | Authorized or approved sourcing channels, incoming inspection, moisture-sensitive-device control, and escalation procedures for shortages or substitutions. | For aerospace and high-reliability programs, assess alignment with AS5553 principles and applicable customer requirements. | Approved supplier list, component authenticity procedure, incoming inspection records, material certificates, and deviation-approval workflow. | 10% | Critical |
| Testing and Product Validation | Coverage of electrical, functional, boundary-scan, flying-probe, in-circuit, programming, burn-in, and environmental tests as required by the product. | Test strategy should be based on design-for-test access, product risk, volume, fault coverage, and customer acceptance criteria. | Test coverage report, fixture-development process, calibration records, test-failure log, golden-unit controls, and sample test data. | 10% | High |
| Industry and Regulatory Readiness | Experience with documentation, validation, change control, and records required by the target market. |
ISO 13485 for medical devices IATF 16949 for automotive supply chains AS9100 for aerospace applications |
Relevant certificate scope, customer-specific requirement process, validation plans, regulatory training records, and change-notification procedure. | 8% | High |
| Reliability and Failure Analysis | Ability to investigate defects, identify root causes, verify corrective actions, and support reliability testing. | Use structured methods such as 8D, root-cause analysis, failure-mode analysis, and controlled corrective-action verification. | Redacted 8D reports, failure-analysis workflow, reliability-test capability, warranty-return analysis, and response-time commitments. | 5% | High |
| Environmental and Materials Compliance | Control of restricted substances, material declarations, supplier declarations, and environmentally responsible manufacturing practices. | RoHS Directive 2011/65/EU EU 2015/863 REACH ISO 14001 | Material declarations, supplier compliance records, laboratory test reports where applicable, waste-control records, and environmental certificate scope. | 5% | High |
| Capacity, Lead Time, and Continuity | Available line capacity, production flexibility, ramp-up planning, alternate equipment, maintenance strategy, and business-continuity readiness. | Evaluate capacity using the buyer’s actual forecast, product mix, changeover frequency, component availability, and required service level. | Capacity model, loading plan, standard and expedited lead times, business-continuity plan, preventive-maintenance schedule, and escalation contacts. | 5% | High |
| Engineering and Design Support | Design-for-manufacturing review, design-for-test feedback, component engineering, PCB layout review, and new-product introduction support. | Review should identify assembly risks involving pad design, component spacing, thermal profiles, test access, solderability, and supply continuity. | Redacted DFM reports, engineering-change examples, NPI stage-gate process, prototype-to-production workflow, and engineering response-time targets. | 4% | Medium |
| Commercial Transparency and Total Cost | Clarity of quotation assumptions, tooling charges, test costs, non-recurring engineering, material terms, yield assumptions, and warranty conditions. | Total cost should include material, assembly, inspection, testing, logistics, tooling, engineering, rework, and lifecycle-support factors. | Line-item quotation, costed bill of materials, payment terms, price-adjustment rules, warranty policy, and documented approval process for substitutions. | 4% | Medium |
Comparing board assembly manufacturers in 2026 requires more than checking unit prices. Experienced buyers should examine process control, engineering depth, and delivery evidence. Ask for recent audit records, production metrics, and sample inspection reports. A clean factory tour helps, but it does not prove long-term reliability.
Review how each manufacturer handles design-for-manufacturing feedback. Strong teams identify solder risks, component shortages, and test access problems before production begins. Request details about automated optical inspection, X-ray inspection, functional testing, and rework procedures. Traceability should connect each board with material lots, operators, machines, and inspection results. Useful proof is specific.
Supply resilience also deserves close attention. Compare approved supplier networks, component authentication methods, and contingency plans for shortages. A manufacturer should explain how it manages obsolete parts and sudden engineering changes. Delivery promises need supporting data, including recent on-time performance and typical recovery times. Low prices can hide weak controls.
Cybersecurity and responsible operations now affect purchasing decisions. Check access controls for design files, employee training, and incident response procedures. Review environmental permits, worker safety practices, and documented quality responsibilities. Certifications are valuable, but they can become paperwork without daily discipline. I have seen polished reports fail to explain simple production delays. That gap deserves uncomfortable questions. Evaluate communication during a pilot run, especially when defects, delays, or unclear drawings appear.
Key factors for comparing board assembly manufacturers in 2026. The chart presents an illustrative 100-point procurement weighting model based on widely used electronics manufacturing evaluation criteria, rather than company-specific performance or market-share data.
Quality and traceability receive the highest weighting because consistent process control, inspection records, and lot-level traceability are essential for reliable board assembly. Engineering support, delivery performance, compliance, cost, and supply-chain resilience should also be assessed using each buyer’s product and risk requirements.
For global buyers, the best board assembly partner in 2026 depends on regional strengths and service design. East Asia remains strong in dense PCB assembly, component access, and high-volume production. European manufacturers often emphasize traceability, engineering support, and regulated-sector quality systems. North American suppliers commonly provide rapid prototyping, local communication, and closer program management. No region wins every time.
Fortune Business Insights valued the global PCB market at about US$89.7 billion in 2023. Its forecast points to continued growth through 2032. WSTS also projected global semiconductor sales would reach US$687.4 billion in 2025. These figures suggest sustained pressure on capacity, lead times, and component planning. A capable manufacturer should offer approved alternatives, automated optical inspection, and clear corrective-action reports. Factory visits still matter. Video tours can hide important details. I would not treat a low quotation as proof of value.
Tips: Match the service model to your order pattern. Choose regional production for prototypes and urgent replenishment. Consider offshore volume production when forecasts are stable. Request sample traceability records, inspection images, and realistic delivery data. Compare total landed cost, not only assembly price.
Selecting a board assembly partner requires more than comparing unit prices. WSTS forecast the global semiconductor market would reach about $611 billion in 2024, with further growth expected in 2025. Rising demand can tighten component availability and production slots. Ask each manufacturer for current lead times, approved-vendor controls, and a documented shortage response plan. Request evidence, not promises.
A capable partner should show traceability from incoming reels to final inspection. Review its quality system, first-article process, solder-paste controls, and inspection coverage. IPC standards provide useful benchmarks for workmanship and acceptance criteria. Also examine defect data, rework rates, and corrective-action records. These details reveal operating discipline.
Do not overlook engineering support. Your partner should review Gerber files, placement drawings, thermal risks, and test access before quotation. A small design change can prevent an expensive production delay. Confirm whether the factory supports SPI, AOI, X-ray inspection, functional testing, and serialized reporting. Logistics matter too: UNCTAD’s 2024 Review of Maritime Transport notes that over 80% of global merchandise trade moves by sea. Ask about regional stocking and customs documentation.
Price still matters. It should not lead alone. One weakness in my own supplier evaluations is trusting polished capability lists too quickly. A live factory audit, sample build, and clear escalation contact provide stronger evidence. Start with a controlled pilot. Measure results.