Electronic Contract Manufacturing Service Provider in California

What Is a Paper Bag Production Line?

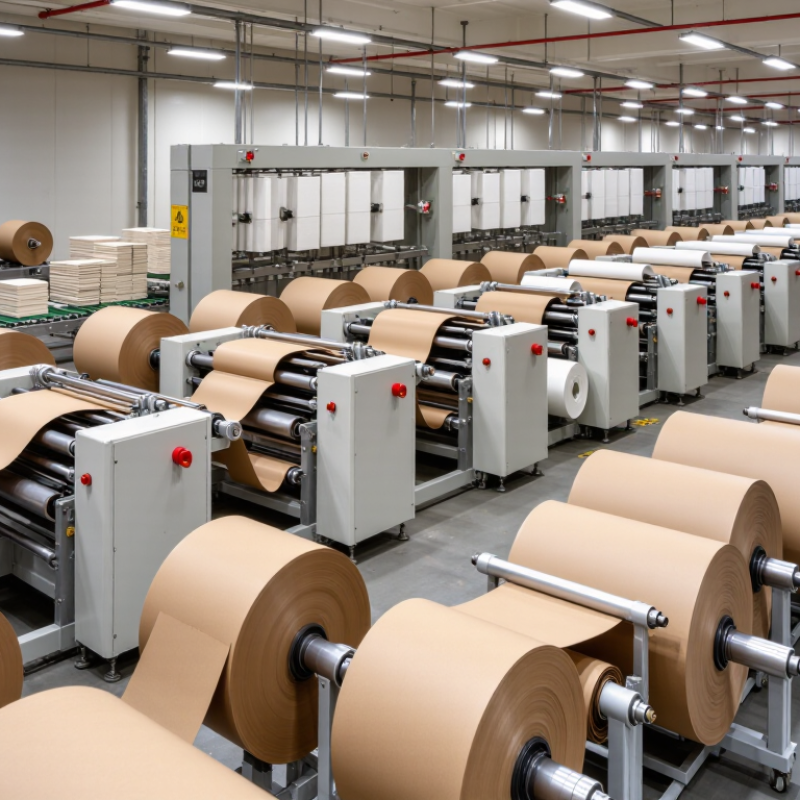
A paper bag production line turns paper rolls or sheets into finished bags through a connected series of feeding, forming, folding, gluing, and cutting operations. Some lines also print designs and attach flat or twisted paper handles. The exact setup depends on bag dimensions, paper weight, handle style, and expected output. In practice, operators may adjust guides and glue settings when changing formats. Small details count.

A Paper Bags Line is not simply one machine running at high speed. It is a coordinated process in which material quality, machine settings, and operator checks all affect the result. Creases must land in the right place, side seams need consistent bonding, and bag bottoms should open evenly. Finished samples are commonly checked for dimensions, print alignment, and handle strength. These checks help identify problems before a full batch is packed.

Automation can reduce repetitive handling, but it does not remove the need for setup, maintenance, or trained supervision. Paper thickness, moisture, and adhesive behavior can influence feeding and bonding. A line’s advertised speed may also differ from its sustained production rate, especially during changeovers or with complex bag designs. That distinction deserves attention. For buyers comparing equipment, useful questions include which bag formats the line supports, how quickly tooling can be changed, and what inspection procedures are available. Understanding these factors makes the production line easier to evaluate and helps set realistic expectations for output and quality.
What Is a Paper Bag Production Line?

Core Definition and Purpose of a Paper Bag Production Line

A paper bag production line is an integrated set of machines that converts paper rolls or sheets into finished bags. It typically unwinds, prints, folds, applies adhesive, forms the tube, makes the bottom, and cuts bags to size. Some lines add handles; others produce handleless bags. Its core purpose is repeatable conversion: controlling dimensions, seam strength, output speed, and material waste across production runs. Operators monitor paper tension and glue application closely. A small shift can wrinkle the paper or weaken a seam. Small details matter. The layout varies with bag style, paper grade, and required output, so one line is not a universal machine recipe.

The environmental purpose needs careful wording. The U.S. EPA’s 2018 Advancing Sustainable Materials Management report states that 45 million tons of paper and paperboard were recycled, a 67.4% recycling rate for that material category. That figure covers paper and paperboard broadly, not paper bags alone. It does, however, show why efficient converting and thoughtful material choices matter. Accurate cutting and stable setup can reduce trim loss, but a production line cannot guarantee a bag will be collected or recycled. It is not automatic. Recovery also depends on local collection systems, contamination, and bag construction. Factory targets are useful, but they should be checked against actual reject rates; sometimes a smooth-looking run still wastes more paper than expected.
Key Machines and Their Functions

What Is a Paper Bag Production Line? Key Machines and Their Functions

A paper bag production line converts a large paper roll into printed, formed, and finished bags. Its first key machine is the unwinder, which feeds paper at a controlled tension. A flexographic printer can add colors, logos, or product information before forming begins. The paper then passes through folding and tube-forming sections, where rollers shape it into a continuous tube and adhesive seals the side seam. Small tension changes matter. Wrinkles can carry through the whole run.

A bottom-forming unit cuts the tube to length, folds its lower edge, and applies adhesive to create a sealed base. For handled bags, a separate station attaches twisted-paper or flat-paper handles. Sensors and operator checks help catch misaligned prints, weak seals, and uneven cuts. This work is practical, not perfect; adhesive settings may need adjustment when paper weight or humidity changes.

FAO’s 2022 Forest Products Yearbook reports global paper and paperboard production of roughly 401 million tonnes. That figure describes a vast material supply, not paper-bag output, but it helps explain why consistent feeding and waste control matter. A few millimeters can spoil a bag.

Paper Selection and Preparation

Paper selection shapes every later stage of a paper bag production line. The choice depends on bag size, filling weight, handle design, and printing needs. A grocery sack needs reliable tear resistance; a small retail bag may prioritize a smooth surface. Check basis weight, stiffness, porosity, and fiber direction against the machine’s forming and gluing settings. Feel matters, but it is not a test.

Scale makes this choice significant. FAO’s Yearbook of Forest Products 2022 reports global paper and paperboard production of roughly 401 million tonnes that year. CEPI’s Key Statistics 2023 reports a European paper recycling rate of about 79 percent. That rate describes recycling, not the recycled-fiber share in any particular paper grade. Recycled furnish can perform well, but fiber quality and strength vary. Ask suppliers for grade specifications and batch consistency, not just a recycled-content figure.

Before converting, inspect the roll edges for damage and verify that the web feeds evenly. Check moisture against the mill’s recommended range; overly dry stock can crack at folds, while damp sheets may wander or wrinkle. Run a short trial with the intended ink, adhesive, and fold pattern. Record defects and adjust tension gradually. It is tempting to blame the paper alone. Sometimes the machine setting is the real problem.

What Is a Paper Bag Production Line? - Paper Selection and Preparation

A paper bag production line converts paper rolls or sheets into bags through processes such as printing, tube forming, bottom folding, gluing, and finishing. Paper requirements vary with bag size, construction, contents, and machine design; the ranges below are general starting points, not universal specifications.

Stage Dimension Typical Material or Practice Why It Matters
Paper selection Paper grade Kraft paper is commonly used for shopping and takeaway bags. Recycled paper may be suitable where its strength, appearance, and intended use meet requirements. Grade influences strength, surface characteristics, print performance, and the bag’s end-of-life options.
Paper selection Basis weight Light-to-medium paper bags often use paper in the approximate range of 70–120 g/m². Heavier-duty designs may require a higher basis weight or reinforced construction. Basis weight affects stiffness and material use, but bag strength also depends on paper grade, dimensions, seams, and handle design.
Paper selection Paper format Automatic lines commonly use rolls; some bag types and production methods use pre-cut sheets. Roll width and core details must match the machine and bag layout. Correct format and dimensions support reliable feeding and reduce trimming or setup waste.
Paper selection Surface and coating Uncoated paper is widely used. Printed, coated, or barrier-treated grades may be selected for particular appearance or product-protection requirements. Surface treatments can affect ink adhesion, folding, and adhesive bonding. Compatibility should be checked before production.
Paper inspection Roll condition Check the roll for damaged edges, telescoping, loose winding, visible contamination, and defects in the paper web. Defects can cause web breaks, feeding problems, poor folds, or visible flaws in finished bags.
Paper conditioning Moisture and storage Keep paper clean, dry, and protected from sudden temperature or humidity changes. Allow wrapped stock to acclimatize to the converting area before use when conditions differ. Paper moisture changes can affect curl, dimensional stability, folding, and feeding behavior.
Machine setup Web width and print orientation Set the roll width and artwork orientation according to the bag dimensions, tube layout, and machine setup. Confirm the print repeats and fold positions. Accurate alignment helps place artwork correctly and ensures the paper folds into the intended bag shape.
Machine setup Web tension and alignment Thread the paper according to the machine instructions, center the web, and use controlled tension appropriate to the paper grade and line speed. Stable tension and alignment help prevent wrinkles, wandering, and uneven folds.
Machine setup Adhesive compatibility Confirm that the adhesive is suitable for the paper surface, coating, and intended seams. Follow the adhesive supplier’s application and curing guidance. Suitable adhesive and application conditions are important for secure side seams, bottoms, and other bonded areas.
Production check Trial run and inspection Run a small trial and check dimensions, folds, print registration, seam bonding, bottom formation, and feeding stability before full production. Early checks help identify material or setup issues before they generate larger amounts of scrap.

Step-by-Step Bag Forming and Finishing

A paper bag production line turns a wide paper roll into formed, finished bags through a series of controlled steps. The roll is mounted on an unwinder, where steady tension helps prevent wrinkles and uneven feeding. If the bag needs printed graphics, printing usually happens before forming. Ink must dry properly; otherwise, it can mark nearby surfaces.

Next, rollers guide the paper into a tube. A narrow strip of adhesive joins the overlapping edges, and forming tools press the seam into place. The tube is cut to the required length, then folded and sealed at one end to create the bag bottom. Small adjustments matter here. A slight shift in the paper path can leave the bottom crooked, even when the seam looks clean.

The open end may be folded into a reinforced rim, while handles are attached if the design calls for them. Handle placement needs consistent spacing so the bag hangs evenly under load. Finished bags are checked for open seams, poor folds, and print defects before bundling. Not every flaw is easy to spot at speed. Operators may need to slow the line or inspect samples by hand, especially after a material change.

Quality Checks and Production Factors

Quality checks begin before the first bag reaches the stack. Operators inspect paper rolls for tears, uneven thickness, and moisture changes. Small differences matter. Damp edges may wrinkle during folding, while brittle paper can split near a glued seam. During setup, crews verify print alignment, cut length, fold position, and adhesive spread. They should test samples at regular intervals, not only at startup. A simple pull test can reveal weak seams. Checking the bottom fold with a filled bag can reveal problems too. Measurements should be recorded because memory is unreliable on a busy shift. Keep records visible.

Production factors shape consistency and material waste. Paper grade, bag dimensions, machine speed, and adhesive settings must work together. Faster output is not always better. If speed rises before the adhesive sets, bags may open during handling. Operators also monitor web tension, blade condition, and temperature near the drying section. A dull cutting edge leaves rough corners; excessive tension can stretch the paper. Some defects appear only after stacking, making inspection awkward. That part is easy to miss. A practical line balances sampling with continuous observation and leaves time for adjustments when the paper lot changes. Even good routines need review; a checklist can become stale.

Paper Bag Production Line: Quality Check Pass Rates

Illustrative results from a sample audit of 1,000 paper bags, not industry benchmarks. Checks cover paper basis weight, moisture, bag dimensions, bottom seals, handle attachment, and print registration. Tracking these results can help identify when material settings or production processes need adjustment.